 PartDorinUpload RFQRFQ
Automotive parts quality control inspection checklist before shipment
A useful inspection plan connects the buyer’s approved product baseline to the actual lot being packed for shipment.
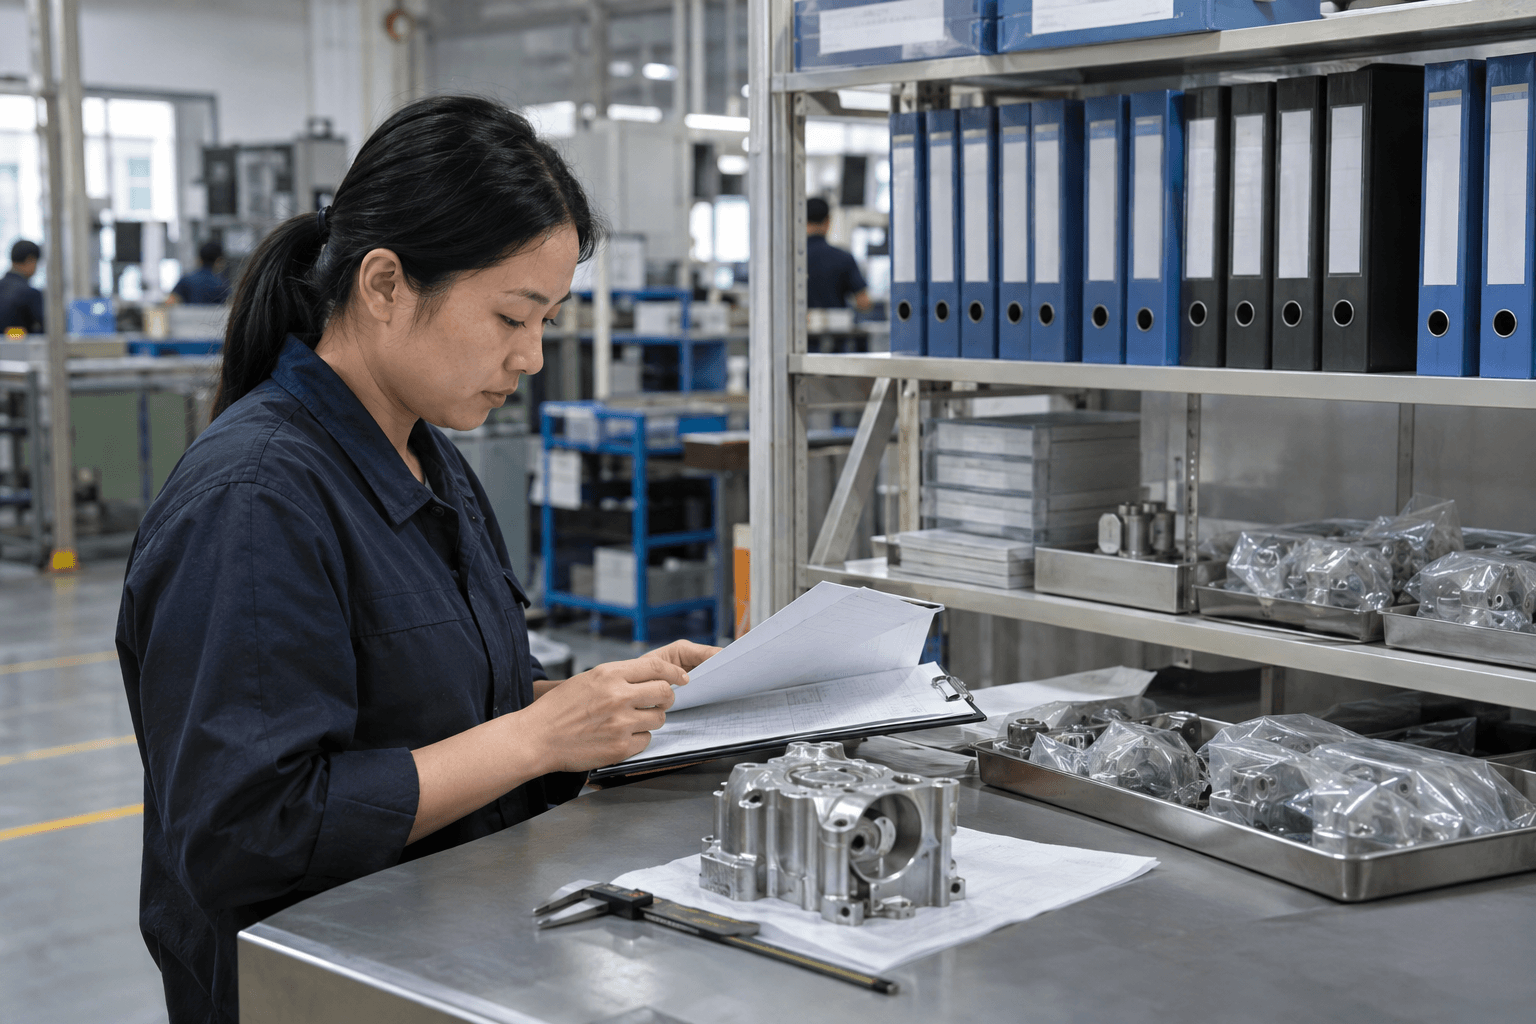
Inspect the characteristics that could change the buyer’s receiving, installation or customer experience: part identity, visual condition, agreed dimensions or function, accessory content, labels, quantity and packing. Define the scope before cartons are closed.
Introduction: inspection starts with the approved baseline
Pre-shipment inspection is most useful when it answers a specific question: does this packed lot match the product, application and presentation the buyer approved? A generic checklist can miss the feature that makes a component usable. A brake disc with the correct finish but the wrong height, a coil with a neat carton but the wrong connector, or a lamp with the right lens but a broken mounting tab can all fail the purchasing purpose. Define the baseline before the inspector arrives.
This guide helps importers, distributors and private-label teams plan practical checks at incoming, production and final stages. It is not a universal acceptance standard. Sampling, test methods and market approvals should be chosen for the part and order by competent technical personnel. The aim is to make the decision clear enough for the buyer, supplier and receiving team to use the same evidence.
Build the inspection file before production
Start with the approved RFQ, purchase order, supplier part number, buyer SKU, vehicle application, drawing or sample record, packaging artwork, accessory list and any category-specific test requirement. Put revision dates on technical documents. If the buyer approved a sample, identify which physical sample or report was approved and what scope the approval covered. A photograph alone may not show dimensions, performance or fitment.
Separate critical from cosmetic characteristics. A mounting interface, connector or brake dimension may determine whether a part can be used. A minor surface mark may affect presentation but not function, depending on the agreed standard. A print color variation may be commercially important for a premium private label but less important for a neutral box. The buyer should define these priorities before the lot exists, so a factory inspector is not forced to invent criteria under time pressure.
For a mixed order, make one inspection line per SKU. The line should specify the expected quantity, product version, packing unit and relevant checkpoints. If one part has a special customer requirement, do not hide it in a general order note. Put it where the inspector can connect it to that part. This is particularly important when several near-identical vehicle variants share a container.
Decide what to inspect at each stage
Final inspection can identify many errors, but it cannot substitute for all earlier controls. Incoming checks may verify material or sourced subcomponent identity. In-process checks may catch incorrect setup, orientation or assembly before a whole batch is completed. Final checks verify product, label, quantity and packing for the released lot. A useful plan assigns each requirement to a stage where correction is practical.
Ask the supplier which tests it performs and under what conditions. “Factory tested” should lead to a method, sample or unit identity, acceptance criterion and record. Some tests are appropriate for every unit; others are sample-based or performed during validation. The right approach depends on the category and customer requirements. A buyer should not ask for a test report that sounds impressive but is unrelated to the part's failure mode.
For a safety-relevant product, validation and regulatory requirements need separate attention. The UNECE replacement braking-parts regulation directory illustrates why brake requirements can be market-specific. Pre-shipment inspection can verify that the approved marking, document and configuration are present; it cannot create an approval that was not obtained.
Check identity and application first
Pick a carton and follow its identity chain. Does the master-carton label match the retail box? Does the retail box match the part marking or identifier? Does that part correspond to the purchase-order line and approved sample? If the product has a lot or serial identifier, can it be linked to the release record? This simple exercise catches many errors before a dimensional check begins.
Where application information is printed, compare it with the buyer's controlled catalogue record. A supplier may have a broader cross-reference list than the buyer approved. The inspector should not silently accept a wider printed fitment claim. Mark the discrepancy and let the technical or commercial owner decide whether the carton needs correction. For product positions such as left/right or front/rear, verify that the physical item and label agree.
Count accessory content against the approved kit bill of materials. A clutch kit without the specified bearing, a pad set without the agreed sensor lead, or a steering assembly missing a connector cover may create an installation delay even if the main component is correct. Photograph the complete kit laid out next to its packing list before the final sample is resealed.
Match category-specific checks to failure modes
For brake discs, inspect the agreed dimensions and construction details using the specified drawing or reference. Depending on the program, surface condition, coating and protective packing may also be important. For brake pads, check backing-plate profile, thickness, sensor and hardware configuration. For wheel bearings, check the hub or bearing type, sensor or encoder features and supplied fasteners. The exact features should be named in the inspection plan.
For ignition and electrical items, inspect connector face, terminal count, housing, boot or harness, visible marking and any agreed functional test evidence. For radiators, verify inlet/outlet arrangement, mounting tabs, fin and port condition, and protective caps. For lighting, check side, connector, lens, mounting tabs and the included module or bulb arrangement. For body panels, surface finish and mounting points deserve explicit attention.
Complex assemblies require a configuration checklist. An engine, transmission or differential may differ by code, ratio, sensors and supplied accessories. Inspect unit labels and interfaces, but also confirm what the order promised. If a test record applies, ensure it identifies the actual version and scope. A generic report for a product family is not the same as evidence for the lot being shipped.
Review packing as part of quality
Packing protects the approved product and identifies the selling unit. Check individual wrap, separators, carton fit, master-carton strength, pallet stability and markings. Heavy or irregular parts can damage lighter cartons when mixed in a container. Fragile lamps and painted panels need protection at vulnerable points; machined surfaces may need appropriate corrosion and contact protection. Inspect the packed sample, not only empty materials or a digital box proof.
Verify carton quantity against the purchase order and packing list. Where barcodes are used, scan examples with the intended receiving workflow. The GS1 guidance on product identification can support a consistent approach to trade-item identification; the buyer still needs to confirm that each printed code maps to its own sellable SKU. An incorrectly mapped barcode can turn a correct shipment into a warehouse problem.
For export shipments, record visible carton and pallet condition before handover. Photographs should include overall pallet views and details of any vulnerable or disputed area. A clean record helps distinguish a production or packing problem from damage that occurred later in transit. It also gives the supplier useful feedback for a revised packing design.
Share the reference, vehicle application and target quantity so the technical and packing questions can be reviewed against your actual order.
Upload Your RFQMake the inspection record usable after the goods arrive
A report should state date, location, order number, inspected SKUs, lot or shipment identity, quantity available, quantity examined, checks performed, results, nonconformities and disposition. For measured characteristics, include the drawing reference and result in the correct unit. For visual findings, include a clear image, description and position on the product. A pass/fail summary without this context is difficult to use if a receiving issue appears weeks later.
Do not represent a sample inspection as proof that every unit was examined. State the sampling method and its limitations. A buyer can choose a larger check for high-risk or first-order lines and a different approach for stable repeat orders, but the decision should be deliberate. If a discrepancy appears, determine the affected scope before approving release. One replaced sample does not establish that the remaining cartons are correct.
Assign a decision owner for exceptions. The inspector records facts; purchasing and the technical authority decide whether to accept, rework, sort, retest or reject. The supplier should document the action and, where appropriate, why the problem occurred. This becomes the corrective-action input for future orders. The PartDorin quality process page describes the broader review and shipment-coordination context.
Use receiving feedback to improve the next plan
Once the goods arrive, compare receiving observations with the pre-shipment record. Were labels readable? Did the carton count match? Did vulnerable parts survive the route? Did installation teams report a configuration difference? Some findings point to the inspection plan; others point to source data, packaging or transport. Classifying the cause matters more than immediately adding every possible check to the next order.
Maintain a short feedback log by SKU and shipment. A repeated wrong connector suggests stronger part identity control. Repeated damaged tabs suggest a packing redesign. Repeated label questions suggest a catalogue or artwork issue. This feedback loop makes inspection more efficient because it focuses on actual risk. It also helps suppliers give a precise response rather than a general assurance.
Illustrative failure investigation: the wrong part in a correct carton
Imagine a shipment in which the retail label and outer carton match the purchase order but the physical connector in one sampled box differs from the approved part. A simple label-count inspection would pass the lot. The inspector should hold the affected stock, identify whether the difference is a supplier version change, a picking error or a catalogue error, and expand sampling according to the agreed disposition process. This is an illustrative inspection scenario, not an assertion that such an event occurred at PartDorin.
The record should show the approved baseline, observed difference, affected SKU and lot, sampled carton positions, photographs and who decides release or rework. Do not relabel the unit based on visual guesswork. If the supplier claims the new connector is equivalent, request technical evidence and decide whether the buyer's application set and customer information need a new approval. An inspector can document a mismatch; engineering or the designated product owner must decide technical interchangeability.
Sampling plans must match risk. Identity and count errors may be checked differently from destructive or laboratory tests. AQL terminology is not a universal promise of zero defects, and a sample pass does not guarantee every piece is identical. The buyer and supplier should agree on inspection stage, sample approach, acceptance and escalation before production. Safety-relevant parts or expensive assemblies may warrant additional controls, depending on the product and target market.
Turn inspection findings into corrective action
When a shipment is accepted with a concession, record precisely which units, deviations, customer approval and time limit are covered. A concession for one batch should not become a silent specification revision. When stock is rejected or reworked, retain traceability so the same units cannot re-enter approved inventory without documented verification. The supplier's response should address root cause and prevention, not only replacement quantity.
Receiving inspection at destination provides a second view of transport and labelling performance. Compare the same critical identifiers used before shipment, then record damage, moisture or carton confusion. If transit damage occurs despite a pre-shipment pass, examine the packed-state evidence and handling route. If a technical mismatch appears in several lots, the baseline or supplier change process needs review. The shipping-damage guide helps distinguish those categories.
Finally, simplify the checklist enough that a real inspector can use it. A long list of generic “check quality” boxes is less valuable than a short set of observable, SKU-specific features with a place for evidence and disposition. Keep the approved sample, drawing, label and test scope accessible at the inspection point. This is the difference between a ceremonial checklist and one that can stop the wrong product from shipping.
What a usable release note should say
The final release note should identify the purchase order, SKU and approved version, lot or batch, sampled quantity, critical characteristics checked, deviations, disposition and who authorized shipment. Attach images that show part identity and decisive features, not only a pallet panorama. If a test result is referenced, state whether it covers the sampled item, batch or design validation. This prevents a buyer from interpreting a one-time laboratory report as routine lot testing.
The supplier and buyer should also agree how urgent findings are communicated before the carrier arrives. A mismatch hidden in a photo folder is not effective escalation. A hold, rework or concession needs a named decision-maker, affected quantity and documented verification step. The same release note can guide destination receiving: staff know which identifiers and pack version to expect. If receiving finds a difference, both teams can compare against a common baseline instead of reconstructing the order from emails.
FAQ
Should every unit be inspected before shipment?
The scope depends on product risk, validation status, process capability and the buyer's requirements. Some characteristics may be checked on every unit during production, while final shipment inspection samples packed goods. The plan should state which is which.
What is the most important inspection photograph?
There is no single photograph. A useful set connects the physical part, its marking, the retail or inner pack, the master-carton label and the order line. Add detailed photos for measurements, defects or vulnerable packing points.
Can inspection replace a sample or fitment approval?
No. Inspection compares a lot against an approved baseline. If the baseline does not establish the intended application or specification, the inspector has no sound basis for declaring the lot suitable.
Conclusion
Effective automotive-parts quality control begins with a defined part and application, assigns checks to the appropriate stage, and ends with a traceable shipment record. Keep inspection proportional to the product, capture exceptions honestly and use receiving feedback to improve the next order. To develop a product-specific plan, send PartDorin your part list and inspection priorities.
Discuss the requirements for your next order.
Send your part references, vehicle applications, target quantities, destination market and any inspection or packing priorities. PartDorin will review the information needed for a focused quotation.
Send Your Requirements