 PartDorinUpload RFQRFQ
How to prevent automotive parts shipping damage in export orders
Most transit problems can be reduced by defining how the actual product, accessories and cartons should be protected before a booking is made.
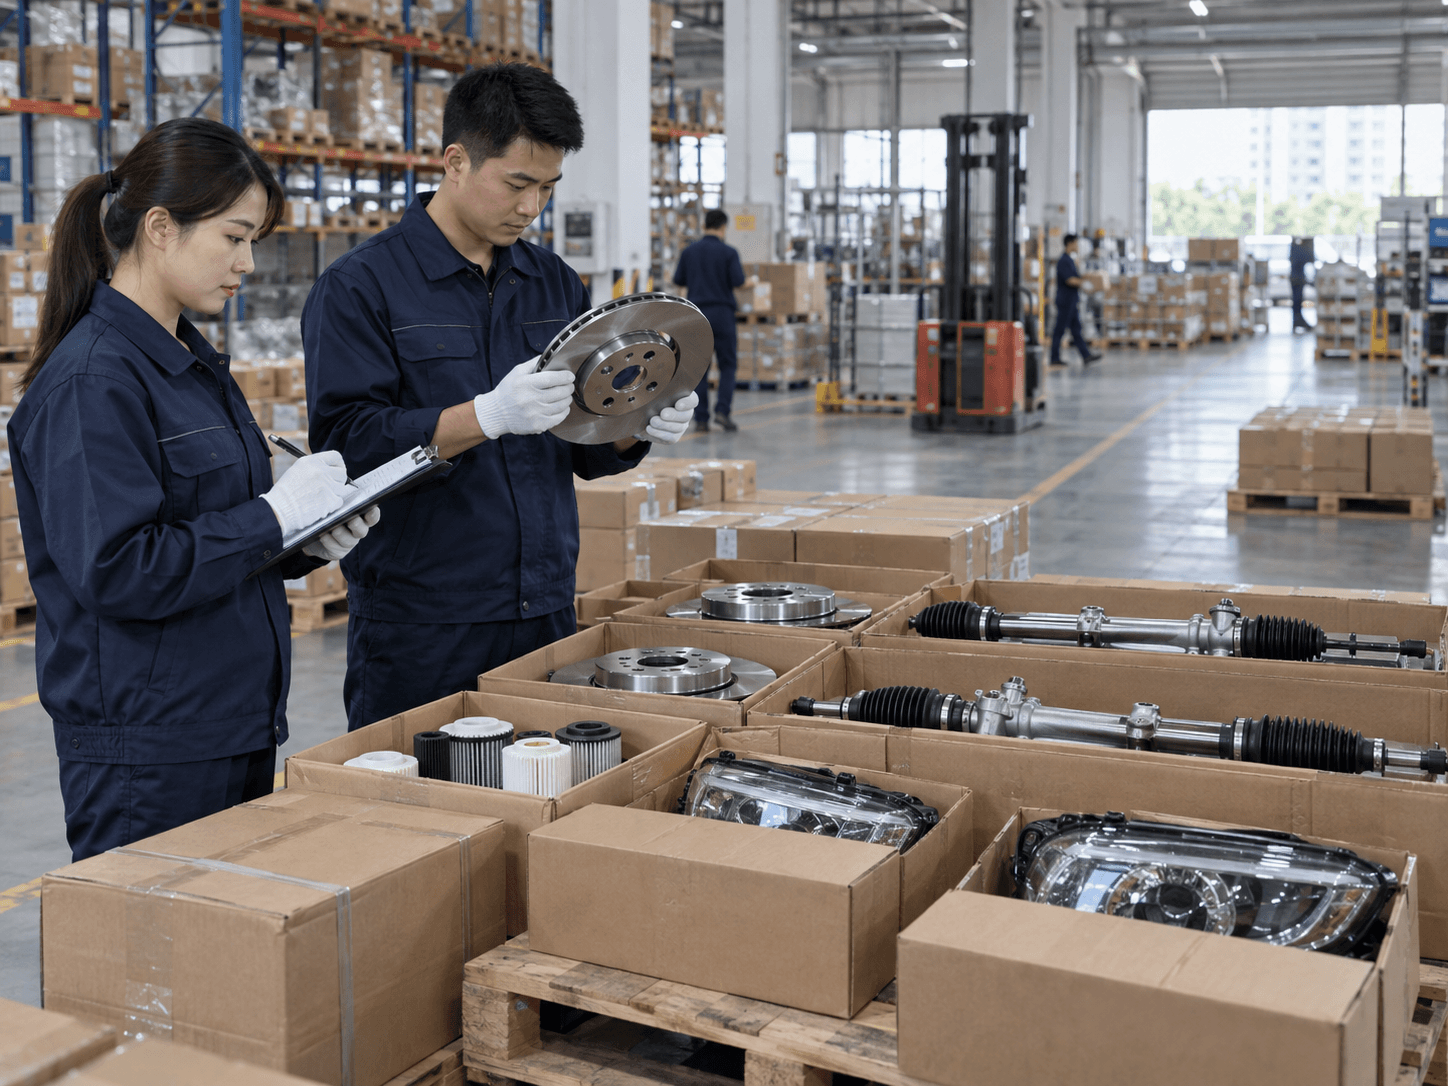
Prevent automotive parts shipping damage by matching protection to the product’s weight, finish, geometry and fragility; then verify the inner pack, master carton, pallet and container-loading plan before release.
Introduction: damage prevention begins with the actual part
Export packing cannot be selected from a catalogue photo alone. Automotive parts vary widely in weight, shape, finish and fragility. A brake disc can abrade a neighboring surface, a headlamp can lose a mounting tab, a radiator can crush a fin or port, and a large assembly can move inside a crate. The correct pack protects the features that make the component sellable and fit for its intended application, then survives the handling sequence to the customer's receiving point.
Damage can occur even when the outer carton appears acceptable. Pressure at one corner, movement inside an oversized box, corrosion during a long route or incorrect stacking can affect a component without obvious exterior marks. This guide provides a buyer's method for specifying, approving and inspecting export packaging for mixed automotive-parts orders. The details should be adapted to the part, route and customer requirements.
Classify each item by damage mechanism
Begin by listing what can be harmed and how. Machined mating faces may need contact protection. Painted panels can scuff or dent. Electrical connectors can bend or collect debris. Fragile lenses and plastic tabs can crack under pressure. Heavy assemblies need restraint and lifting information. Small accessory bags can be lost in a large carton. A useful packing specification names these vulnerabilities rather than asking for “strong export packing.”
Group the order into practical classes: heavy machined parts, long or irregular parts, fragile optical or plastic parts, sensitive electrical items, finished body surfaces and small service kits. For each class, identify the key surfaces and the handling method the destination warehouse will use. A product that arrives intact but cannot be safely unloaded or matched to its SKU still creates a commercial problem.
Do not assume that similar-looking parts need identical packs. A coated brake disc and an uncoated disc may have different surface-protection needs. A radiator with protruding plastic ports has different pressure points from an all-metal unit. An engine assembly supplied with sensors may need interface protection that a bare short block does not. Packing must follow the approved product configuration.
Map the full handling route
The pack may be moved at the factory, stacked in a staging area, loaded onto a truck, transferred to a port, carried by sea or air, cleared through customs and handled again at the destination. Each transfer creates vibration, impact and stacking conditions. Ask whether the goods will be palletized, containerized or consolidated with other suppliers' cartons. State any loading orientation and maximum stacking assumption that the packing design relies on.
Destination receiving matters. A buyer using forklifts, pallet jacks or manual unloading may need different pallet dimensions, carton weights and labels. A mixed container with many SKUs needs a packing list and marks that allow an efficient count without opening every box. A plan optimized only for container space can shift the cost to damaged goods or slow destination sorting.
Discuss humidity and storage duration where they are relevant. Metal surfaces may need an agreed corrosion-prevention method, while paper packaging or labels may need protection from moisture. Do not add an unspecified chemical or film to a product that will be installed in a sensitive application. Identify the method, any removal instruction and the approval owner.
Design the layers: part, inner pack, carton and pallet
The first layer should keep vulnerable surfaces from touching hard or abrasive materials. Use caps, sleeves, separators or shaped inserts where the product needs them. The inner pack should prevent movement without placing pressure on delicate features. The master carton should resist the expected load and keep contents from shifting. A pallet or crate should provide stable handling and protect cartons from crushing during transport.
For heavy components, check the package against the actual unit weight and geometry. A part may be within the carton weight rating but still punch through a weak base because its load rests on a small edge. For long shock absorbers or shafts, protect both ends and restrain the item lengthwise. For body parts, protect corners and mounting tabs independently of the broad surface. For lamps, a snug box that presses on the lens or tabs can be worse than a slightly larger, well-supported one.
Use a packed physical sample to assess contact points. Close the box, lift it as a handler would, rotate it carefully and inspect whether the part shifts or bears against the carton. The review need not be an elaborate laboratory program for every SKU, but it should be deliberate. If the product is high-value or has a known damage pattern, the buyer can specify additional packaging validation with competent logistics and quality staff.
Specify carton data and labels clearly
Each package should identify the correct buyer SKU, supplier part number, product description, quantity and any orientation or handling marks that are actually needed. For a private-label program, verify that artwork revision and barcode match the approved sellable unit. GS1 product identification guidance can inform barcode planning; the warehouse still needs to test that the code scans into its own system and points to the right SKU.
Outer carton marks should support receiving and discrepancy investigation. A mixed shipment needs carton counts by line, not just a total box number. The packing list should map cartons or pallets to purchase-order lines. If several products share a master carton, the inner packages must be separated and identified in a way the destination team can maintain after the carton is opened.
Handling marks should be meaningful. “Fragile” does not replace a suitable package. “This side up” may be ignored in real transit; the pack should be designed for likely orientation changes unless the transport plan reliably controls orientation. Likewise, a maximum stack height is useful only when it is communicated to the people who load and store the goods.
Plan mixed loads to prevent cross-damage
When loading a mixed container, place heavy, stable goods so they cannot crush lighter or fragile cartons. Protect painted panels and lamp cartons from hard edges and shifting assemblies. Account for weight distribution, load restraint, aisle or access needs and the unloading sequence at destination. A dense load is not a successful load if the first pallet cannot be moved without damaging the cartons behind it.
Agree how different factories' goods will be consolidated. If a freight partner repacks cartons or removes pallets, the buyer should know whether the approved protection remains effective. Photograph the condition before and after a handover where feasible. A clear chain of custody helps distinguish original packing weaknesses from later damage and gives practical evidence for future changes.
Do not calculate container fit from nominal carton dimensions alone when irregular parts or overhanging pallets are involved. Request actual packed dimensions and gross weights. Compare the proposed plan with the product's stacking limitations, not just with the container's empty cubic capacity.
Share the reference, vehicle application and target quantity so the technical and packing questions can be reviewed against your actual order.
Upload Your RFQInspect packed goods before release
Pre-shipment inspection should review a packed sample from the production lot. Open selected boxes and check the product, protective materials, position, accessories and label. Then review master cartons, pallet stability, wrapping or strapping, marks and the packing list. For fragile or heavy lines, select samples from more than one position in the staged lot. Record any carton damage and determine whether it was isolated or repeated.
Photographs should show the actual product in its inner protection, the closed retail or neutral pack, master carton and completed pallet or crate. A product image outside the box does not demonstrate that the export pack is adequate. If a defect is found, correct the relevant scope before release. Replacing one photographed box while leaving the same design in the rest of the shipment does not solve a systematic issue.
The PartDorin manufacturing overview and quality process can be used to discuss packing and final-check priorities for a specific product list. A buyer should provide destination, transport mode, pallet preference and any known damage history before production packing begins.
Use receiving evidence to improve the next shipment
At destination, record the condition of the container, pallets, cartons and affected parts before repacking or disposal. Note the position of damaged goods in the load. Photograph the outer and inner protection, product marking and carton label. This allows a cause review: impact, crushing, movement inside the box, moisture, abrasion or a picking problem may require different actions.
Track damage rate by SKU and packaging revision rather than only by shipment total. A recurring cracked lamp tab calls for a revised insert or tab clearance. A scuffed body panel may need a different separator. A damp carton may point to handling or moisture protection. A mislabeled carton is a data-control issue, not a cushioning issue. A specific cause produces a useful requirement for the next RFQ.
Illustrative diagnosis: crushed cartons versus damaged parts
Suppose an importer finds several crushed cartons at a pallet edge while the parts inside remain sound. The immediate response differs from a shipment where outer cartons look intact but radiator ports or lamp tabs are broken. In the first case, review pallet overhang, stacking and external handling. In the second, inspect the inner restraint and pressure points. Both findings matter, but “shipping damage” is too broad to guide a useful change. This example is a diagnostic framework, not a PartDorin shipment claim.
Record the original pallet, carton and inner-pack condition before repacking. Photograph the damage location with the part and SKU label visible. Note whether the issue is concentrated at the top layer, pallet edge or one carton orientation. A consistent pattern may identify a design or loading weakness. Random severe impact may indicate a different transport event. The claims process should preserve evidence for supplier, carrier and buyer without assigning blame before the facts are clear.
When evaluating a new pack, check the actual product's vulnerable features. A brake disc needs face and edge separation; a radiator needs fin and port protection; a steering rack needs restrained mass and capped openings; a lamp needs protection for lens and mounting tabs. A generic “foam insert” line on a quote is not a specification. Ask for a packed sample and define whether a handling or compression test applies to that part and route. Do not extrapolate a package result from one component to every shape in the catalogue.
Make packaging control repeatable across orders
Store a pack revision with the product SKU and approved sample. The production and warehouse teams should know insert position, carton orientation, allowable mix, pallet pattern and label location. If material thickness or carton supplier changes, evaluate whether the original approval still applies. A pack change is easy to overlook because the product itself is unchanged, yet it may alter damage performance materially.
At shipment inspection, sample from different pallet positions and compare the actual pack with the approved revision. Count protective pieces, verify that parts cannot move into fragile features, and check that labels remain legible after wrapping. At destination, use the same vocabulary to report damage: dented housing, bent port, abraded finish, broken tab, moisture or crushed carton. This allows buyers to analyze patterns instead of aggregating every issue into one “damaged” category.
The commercial review should consider pack cost alongside freight cube, labour, storage and claims. A more expensive inner support may reduce returns, while an oversized box may increase freight with little benefit. Use observed receiving results from the first shipment to revise the pack; do not assert a universal percentage reduction without controlled data. The body-parts export guide applies this method to large fragile panels.
A pack approval sheet that travels with the order
For each high-risk item, keep a pack approval sheet showing the part and selling unit, vulnerable features, inner restraint, carton or crate specification, pallet position and permitted substitutions. Add photographs taken during assembly of the pack, not only after closure. If a supplier switches to a new insert or box because material is unavailable, the buyer can see which protection function might change and decide whether to repeat a trial.
Put the pack version on the purchase order and inspection instruction. At the loading stage, compare the planned pallet pattern with the actual mix of heavy and fragile goods. At destination, use the same sheet to inspect a damaged item and record exactly which layer failed. This shared reference makes a claim more objective and turns a one-off loss into a controlled improvement to the next shipment.
FAQ
Are pallets always required for automotive export shipments?
No. The appropriate method depends on product size, route, unloading equipment, space and destination requirements. The buyer should agree the planned method and verify that protection remains suitable for that method.
How can I compare two packing proposals?
Compare the protected surfaces, movement restraint, inner and master-carton construction, pallet method, total dimensions, weight, labeling and likely destination handling. A cheaper pack should be judged against the cost of damage and receiving work.
What should I do if the outer carton is intact but a part is damaged?
Retain the part and all packing layers, photograph contact points and record the carton position. The cause may be internal movement or concentrated pressure, which will not necessarily mark the outer box.
Conclusion
Export packing is a product-specific control. Identify the vulnerable features, map the handling route, approve a packed sample, inspect the released lot and learn from destination evidence. A clear packing requirement gives both buyer and supplier a better chance to prevent repeat damage. For a mixed parts shipment, send PartDorin your product list and destination packing needs.
Discuss the requirements for your next order.
Send your part references, vehicle applications, target quantities, destination market and any inspection or packing priorities. PartDorin will review the information needed for a focused quotation.
Send Your Requirements